Conventional NDT Services
Eddy Current
Testing
- Laboratory & on-site inspection
- Clear, traceable reporting
- Fast scheduling
Inspection Snapshot
Fast electromagnetic inspection of conductive materials
Surface & Weld Examination
Rapid scanning for cracks and local discontinuities
Tube & Component Inspection
Heat exchanger tubes, aircraft parts and precision components
Conductive Material Analysis
Aluminum, copper, stainless steel, nickel alloys and other conductive metals
Discuss your inspection
Certified Personnel
Qualified NDT professionals
Fast Turnaround
Responsive scheduling
Modern Equipment
Calibrated UT instruments
Detailed Reports
Clear inspection findings
Rapid & Sensitive
Inspect conductive components with minimal disruption.
 What is eddy current testing?
See small defects through electromagnetic response
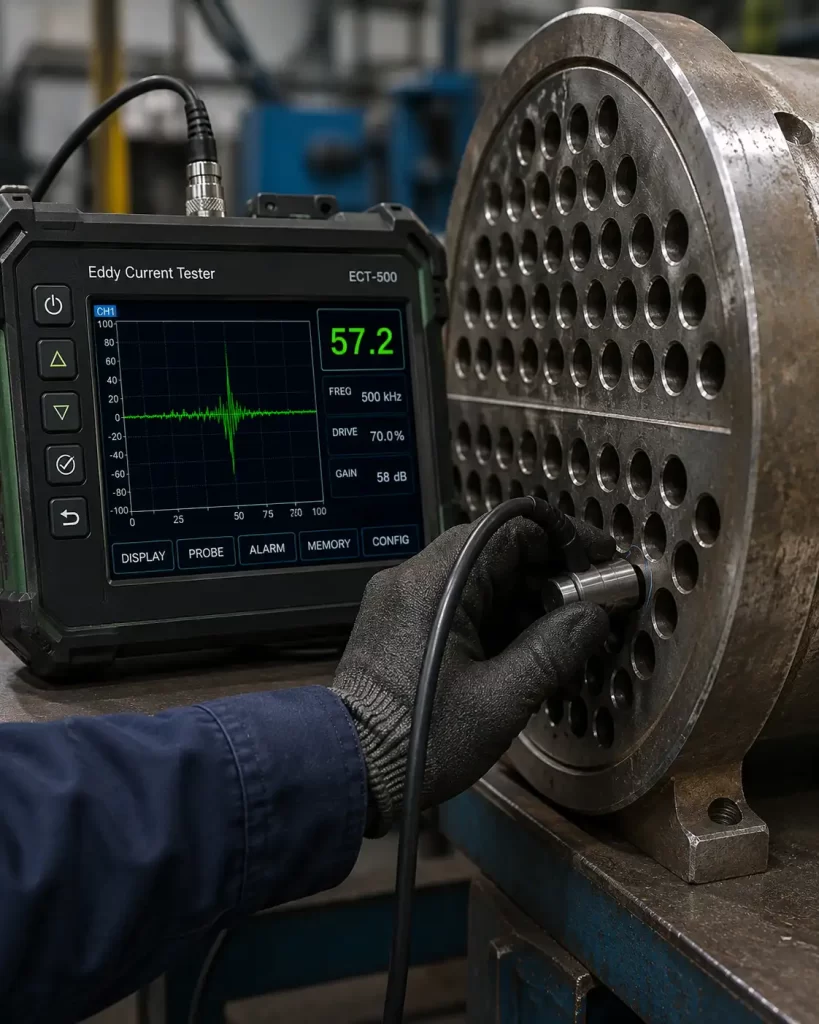
Eddy Current Testing (ECT), also called Eddy Current Inspection, is a non-destructive electromagnetic method used to examine electrically conductive materials for surface and near-surface discontinuities, corrosion, wall loss and changes in material condition.
An alternating current energizes a probe coil and produces a changing magnetic field. When the probe is brought near the component, circulating electrical currents are induced in the material. Cracks, thinning, conductivity changes and geometry variations disturb these currents, producing signals that are interpreted by a qualified inspector.
Surface crack detection
Near-surface flaws
Tube wall loss
Corrosion assessment
Conductivity sorting
Heat exchanger tubing
--------- Our Process ---------
A controlled electromagnetic inspection from setup to report
Every job is planned around the material conductivity, component geometry, probe access,
expected defect orientation, inspection frequency and applicable acceptance criteria.
Scope Review
We review the material, geometry, coating condition, probe access, expected discontinuities and applicable acceptance criteria.

Calibration & setup
The instrument is configured using suitable probes, frequencies and reference standards for the material and inspection objective.
Scan & Acquire Signals
The probe is moved systematically across the inspection area or through the tube while electromagnetic responses are recorded.
Evaluation & Report
Relevant signal responses are interpreted, documented and compared with reference indications and applicable acceptance criteria.
--------- Inspection capabilities ---------
Eddy current inspection for conductive components
Our ECT services support manufacturing quality control, heat exchanger and condenser tube inspection,
weld examination, corrosion monitoring, material sorting and failure investigations.
Weld & Surface Inspection
Scan welds, heat-affected zones and accessible surfaces for fatigue cracks and other surface or near-surface discontinuities.
Heat Exchanger Tubes
Inspect non-ferromagnetic tubing for pitting, wall loss, erosion, cracking and support-related indications.
Precision Components
Evaluate machined parts, fastener holes, shafts, wheels and high-value components for cracks or localized material changes.
Conductivity & Material Sorting
Compare conductivity response to support alloy sorting, heat-treatment verification and detection of localized material variation.
In-Service Inspection
Inspect conductive components in service for corrosion, fatigue cracking and deterioration with minimal surface preparation.
Coating & Thickness Applications
Measure non-conductive coating thickness on conductive substrates or evaluate thin material sections where the application permits.
--------- Discontinuities ---------
What eddy current testing can detect
Surface Cracks
Near-Surface Cracks
Fatigue Cracks
Tube Wall Loss
Pitting Corrosion
Erosion
Weld Discontinuities
Conductivity Changes
Material Mix-Ups
Coating Thickness
--------- Codes & standards ---------
Inspection aligned with your requirements
Testing can be performed to applicable customer procedures, drawings, specifications and recognized industry standards. The final technique is confirmed after reviewing material conductivity, permeability, geometry, probe access, coating condition, reference standards and acceptance criteria.
ISO 17643
Eddy current testing of welds
ASTM E243
Copper-alloy tube examination
ISO 15549
ECT general principles
ASME V
Article 8 requirements
Client Spec.
Project requirements
ASTM E426
Tubular product examination
--------- Industries served ---------
Supporting quality, safety and asset integrity

What our clients say
Posted on Google
 Paul Herman
Trustindex verifies that the original source of the review is Google.
Thank you for the quick service and the complete report. Best wishes Paul Herman Firwin CorpPosted on Google Jon HimelfarbGreat service, above and beyond what was asked for or expected. CMH Metlabs expedited their internal processes to meet an urgent request and helped us meet our deadlines. 100% would recommend them.Posted on Google
 Mark NowakowskiThank you CMH METLABS for your attention, professionalism and responsive communication. This includes your extra follow-up to confirm the lab test results. We were able to continue our business with minimal delay thanks to your efforts!Posted on Google
 George BertonVery co operative with information and timing.Posted on Google
 ahmadreza asefiThe professional team, the good testing equipment, the short turnaround time, and the comprehensive reporting have all made us extremely satisfied with this laboratory. We will certainly return to them for future testing needs.Posted on Google
 Etienne FortierSubmitted metal sampled for testing, obtained test results promptly and professionally. Highly Recommended.Posted on Google
 Sanjay SharmaBirla Carbon Hamilton worked with CMH for testing their boiler tube . CMH Metlabs issued a report for their testing. The report was good and covered all technical requirements. We will work with them in future.Posted on Google
 Don Webster
Trustindex verifies that the original source of the review is Google.
CMH Metlabs did a number of chemical analysis for us over the last few weeks. The prices are good and the turn-around time was excellent. We needed some clarity on the results from the tests. The technical people at CMH responded quicky and our questions were answered. We discovered a couple of typos in the reports but it did not affect the over all accuracy of the report. We are looking forward to continuing our analyses with CMH.
Frequently asked questions
Answers before you schedule
Does eddy current testing damage the component?
No. Eddy current testing is non-destructive and normally requires little or no surface preparation. The probe does not alter the component during inspection.
What materials can be inspected by eddy current?
Can testing be completed on-site?
What information is needed for a quotation?
How deep can eddy current testing detect?
--------- Need an inspection? ---------
Detect hidden deterioration before it affects performance
Contact CMH Metlabs
Plan your eddy current inspection
- Phone: 647-365-0906
- Email: info@cmhmetlabs.com
- Service Area: Ontario and across Canada
- Availability: Laboratory and on-site services
Tell us about your job
By submitting you agree to be contacted about your request. We never share your details.